How Semiconductor Material Analysis Powers Modern Tech
Key Physical and Chemical Methods in Semiconductor Material Analysis
Understanding modern microelectronics requires tools capable of inspecting atomic arrangements, chemical states, and trace contamination. Advanced physical and chemical characterization tools allow us to pinpoint material deviations before they turn into costly manufacturing failures.
When analyzing thin films and micro-scale structures, tools like micro-spot Energy Dispersive X-ray Fluorescence (EDXRF) provide rapid, non-destructive elemental composition and film thickness measurements. Systems such as Micro-spot EDXRF metrology tools deliver a beam spot size down to 10 µm with polychromatic optics, enabling target analysis on wafers up to 300 mm. Using a helium atmosphere alongside specialized Silicon Drift Detectors (SDD), EDXRF can detect light elements like carbon, oxygen, magnesium, aluminum, and phosphorus.
To evaluate chemical bonding environments and deep interfaces, X-ray Photoelectron Spectroscopy (XPS) measures core-level electron binding energies. Standard Al Kα sources probe the uppermost few nanometers, while Hard X-ray Photoelectron Spectroscopy (HAXPES) using a Cr Kα source probes approximately three times deeper. This non-destructive depth profiling reveals chemical oxidation states at buried interfaces without requiring aggressive ion beam sputtering.
When absolute elemental distributions are needed across three dimensions, Time-of-Flight Secondary Ion Mass Spectrometry (ToF-SIMS) offers sub-ppm sensitivity with a lateral resolution of a few hundred nanometers and a depth resolution of a few monolayers. Furthermore, inside scanning transmission electron microscopes, quantitative Energy-Dispersive X-ray Spectroscopy (STEM-EDX) evaluates localized compositions. Advanced quantification strategies, such as internal composition determination (ICD), eliminate the need for external standards by leveraging a known stoichiometric element in a reference region. This approach quantifies ternary semiconductor alloys (such as AlGaAs, GaAsSb, or InGaN) within 3.9 at% accuracy compared to standard calculated k-factors.
X-Ray and Electron Spectroscopic Methods in Semiconductor Material Analysis
X-ray scattering and spectroscopic measurements provide structural insights into crystal matrices and multilayered stacks. X-ray Diffraction (XRD) measures crystalline phase, crystallographic orientation, and lattice strain. High-resolution reciprocal space mapping evaluates pseudomorphic strain in epitaxially grown SiGe layers, ensuring lattice matching remains intact.
X-ray Reflectometry (XRR) provides precise, non-destructive thickness, density, and interfacial roughness measurements for thin films ranging from 1 nm to over 100 nm. Meanwhile, XPS resolves chemical bonding states in high-k gate dielectrics and native oxide layers. For detailed guidance on picking the best depth-resolved characterization technique for your specific stack, review our Depth profiling techniques guide.
ToF-SIMS excels at tracking dopant diffusion profiles, trace impurities, and interface segregation across complex stacks like Ti/TiN/HfO2 in Resistive RAM (RRAM) devices.
High-Resolution Microscopy and 3D Atom Probe Tomography for Semiconductor Material Analysis
Physical failure analysis often relies on direct visual and structural mapping at sub-nanometer resolutions. Scanning Electron Microscopy (SEM) provides top-down surface defect screening, identifying micro-cracks, surface contamination, and wire bond degradation. When internal features require inspection, Focused Ion Beam (FIB) systems mill site-specific cross-sections and extract electron-transparent lamellae (20 to 100 nm thick) with sub-10 nm placement precision for TEM analysis.
For complex 3D architectures like gate-all-around (GAA) nanosheets or FinFETs, 2D TEM imaging faces limitations due to overlapping feature projections. Advanced 3D electron tomography reconstructs full volume models to map nanoscale variability in feature length, interface roughness, and structural defects.
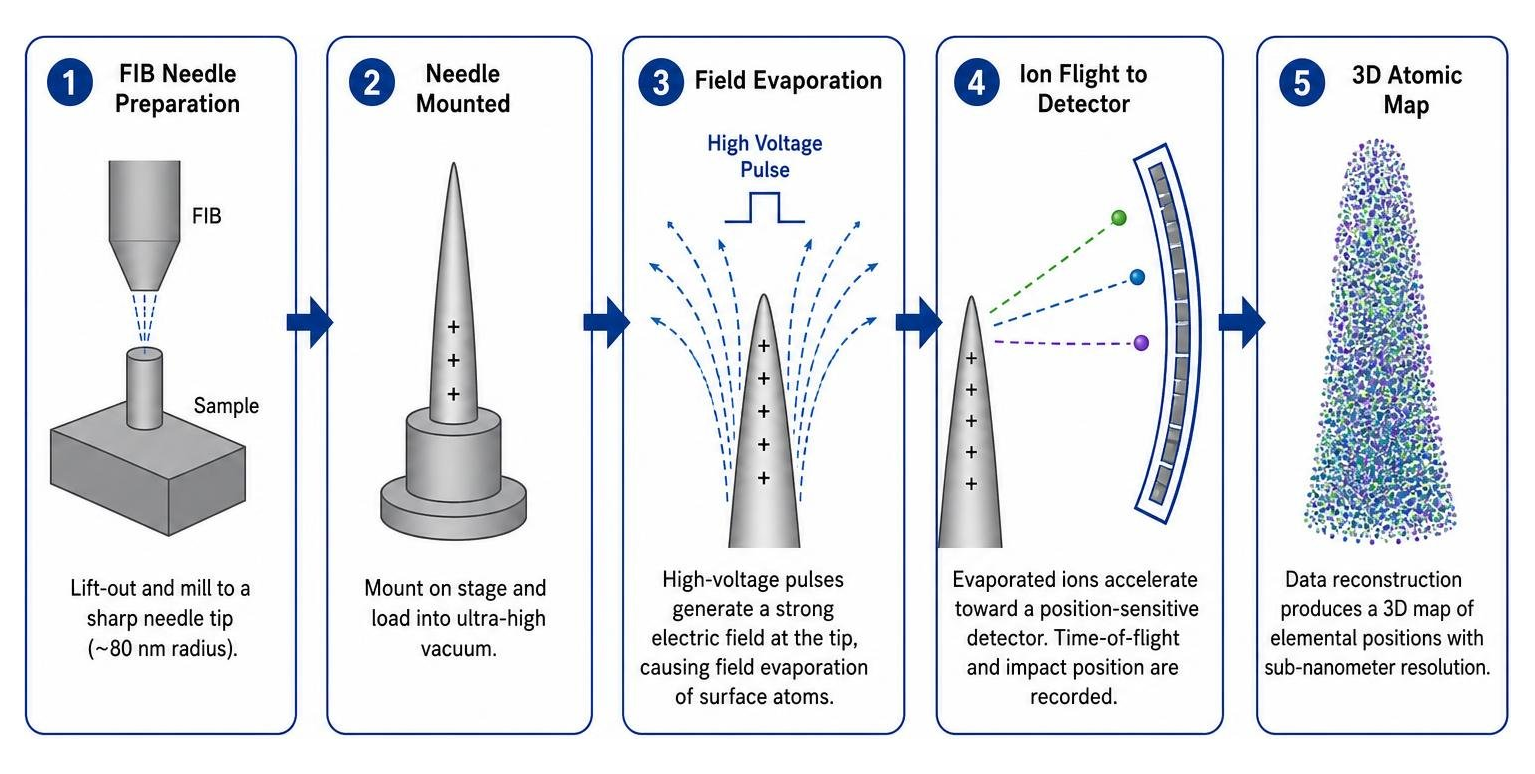
At the ultimate nanoscale limit, Atom Probe Tomography (APT) delivers sub-nanometer 3D isotopic distribution mapping. The specimen is shaped into a sharp needle with an apex radius near 80 nm using FIB liftout. Kept under high vacuum ($10^{-8}\text{ Pa}$) at cryogenic temperatures (~50 K), high-voltage pulses trigger field evaporation, extracting single ions toward a time-of-flight position-sensitive detector. As detailed in this 3D atom probe analysis application note, APT achieves over 75% atomic identification efficiency in 3D, making it vital for analyzing source/drain dopants, silicide interfaces, and nanoscale contacts.
To complement mass profiling with physical strain monitoring, Raman spectroscopy maps mechanical stress and active device temperatures non-destructively with sub-micron spatial resolution by measuring inelastic light scattering.
Wafer-Level Testing, Automated Metrology, and Inline Quality Control
Catching processing errors on raw wafers prevents wasting packaging resources on defective dies. Wafer-level testing subjects un-encapsulated dies to functional screening, while inline metrology verifies pattern dimensions, layer thickness, and surface roughness inside cleanrooms matching Class 1000 (ISO 14644-1 Class 6) standards.
Automated Test Equipment (ATE) interfaces with probe cards to evaluate thousands of individual dies per hour. High-speed CD-SEM platforms, such as Critical dimension SEM metrology solutions, deliver high fleet-matching precision to track feature dimensions from 0.1 µm up to over 100 µm across 150 mm, 200 mm, and 300 mm wafer formats. Advanced inline analytics align with strict industrial quality protocols, similar to those outlined in 300 mm wafer analytics standards.
| Testing Stage | Primary Objectives | Typical Test Methods | Key Advantages |
|---|---|---|---|
| Wafer-Level Testing | Screen bare dies, identify early life failures, classify yield | Electrical Die Sorting (EDS), Wafer-Level Test & Burn-In (WLTBI), CD-SEM | Prevents packaging defective silicon; enables laser re-processing/repair |
| Final Package Testing | Verify device assembly, wire bonds, encapsulation, and final performance | Automated Test Equipment (ATE), Thermal cycling, Shorts/Opens/Leakage screening | Assures environmental durability, interconnect integrity, and full device compliance |
Electrical Die Sorting, Shorts, Opens, and Leakage Tests
Electrical Die Sorting (EDS) uses fine probe needles to make direct contact with die pads on the wafer.
- Shorts and Opens Testing: Checks for unwanted continuity between adjacent lines or broken conductive traces.
- Leakage Current Measurement: Evaluates parasitic drain currents across gate oxide layers to detect dielectric degradation.
- Device Orientation Verification: Ensures correct pin alignment and symmetry before packaging assembly.
When non-fatal defects are identified, repairable memory chips can be mended on-wafer via laser fuse-blowing (re-lasering repair) followed by re-testing to recover die yield.
Inline Metrology vs. Final Package Testing
Inline metrology tracks high-throughput process stability during wafer fabrication without destroying functional circuits. Techniques include 3D Atomic Force Microscopy (3D-AFM), spectroscopic ellipsometry, and non-contact sheet resistance mapping.
Once wafers are diced, mounted, and encapsulated, final package testing validates the completed microelectronic component under real-world conditions. ATE units exercise device pins across dynamic clock speeds and operational temperature ranges. For a detailed breakdown of fundamental testing equipment and laboratory practices, check out our Elemental testing laboratory introduction.
Advanced Defect Characterization: Thermal Resistance and Subsurface Profiling

As chip power densities rise, managing heat dissipation across sub-micron material interfaces becomes just as important as managing electrical conductivity. Thermal resistance bottlenecks cause hot spots, localized stress, and early device degradation.
Traditional contact methods for measuring thermal resistance struggle with interface contact impedance and sub-micron spatial limitations. To overcome these issues, advanced optical methodologies isolate bulk thermal conductivity from interfacial resistance without contacting the wafer surface. For an overview of specialized physical characterization tools, read our Nanomaterial characterization practical guide.
Non-Contact Thermal Resistance Measurement Techniques
Steady-State Thermoreflectance in Fiber Optic (SSTR-F) configurations offers a non-contact laser technique for thermal characterization. By directing a continuous-wave pump laser onto a thin metal transducer layer, SSTR-F creates localized heating and monitors the resulting reflectance shifts using a probe laser.
This methodology delivers accurate, reproducible measurements of bulk thermal conductivity and interfacial thermal resistance across complex material stacks (such as SiC-to-GaN or metal-to-dielectric bonds). Non-contact thermoreflectance allows engineers to screen for interfacial delamination, void formation, and bond line defects early in development.
FIB-SEM Failure Analysis and Cross-Sectional Profiling
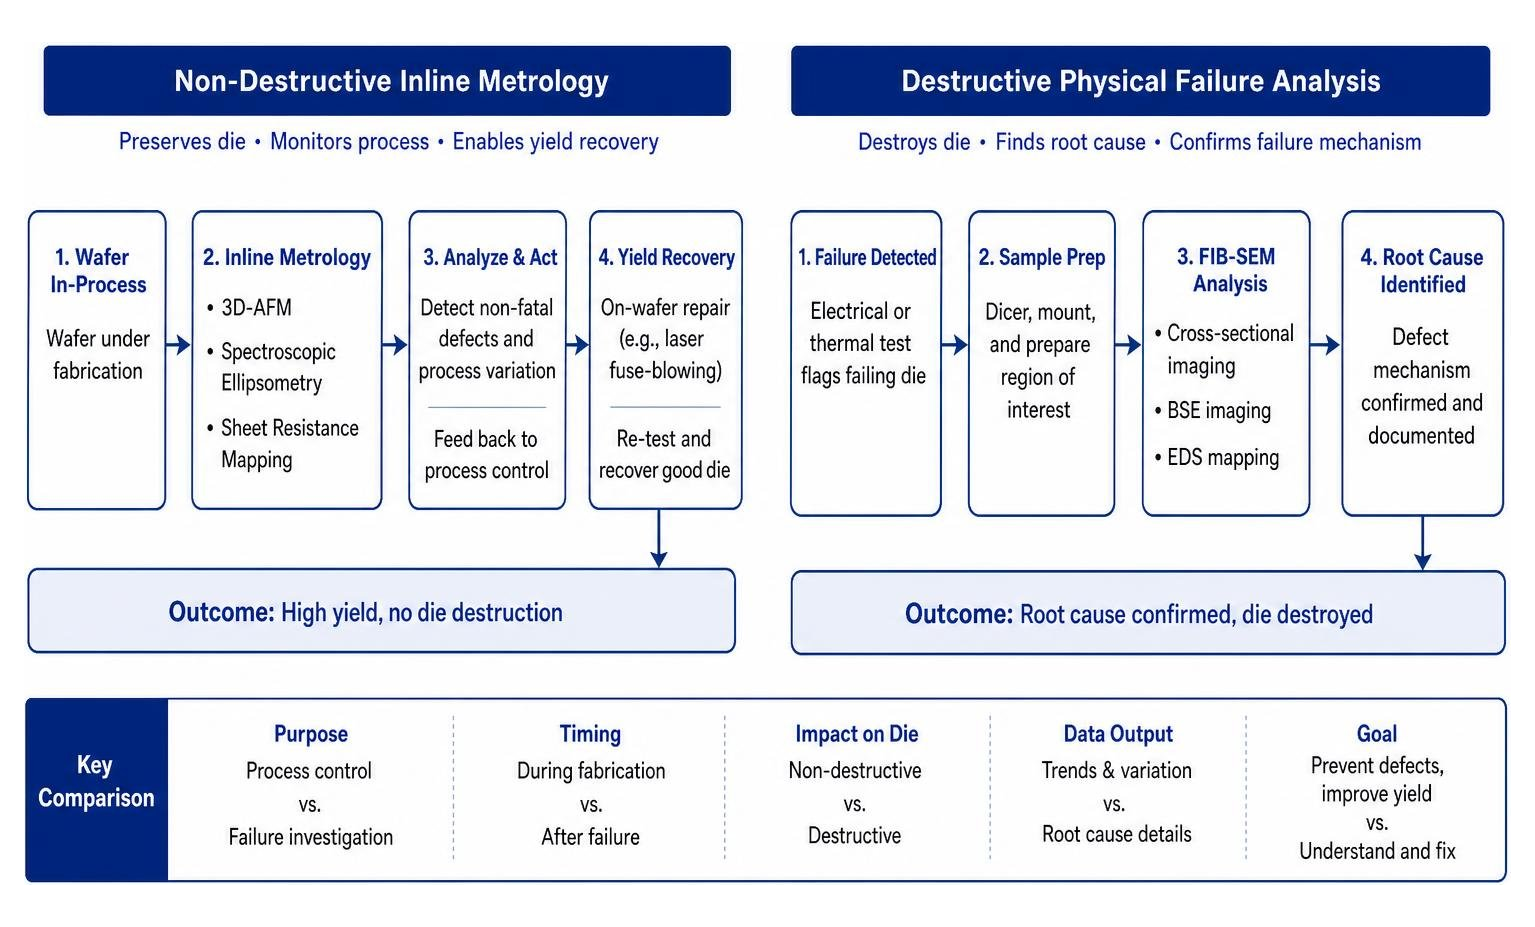
When electrical or thermal testing flags a failing die, physical failure analysis locates the root cause. Dual-beam FIB-SEM tools use ion beams ($Ga^+$ or plasma sources) to cut precise cross-sectional trenches directly through flagged defect locations.
- Cross-Sectional Surface Inspection: Reveals subsurface voiding, dielectric breakdown channels, and keyhole formation in high-aspect-ratio vias.
- Wire Bond and Packaging Inspection: Backscattered electron (BSE) imaging highlights intermetallic compound formation, Kirkendall voiding, and micro-cracking at wire-bond contacts.
- Surface Contamination Tracking: Energy-Dispersive X-ray Spectroscopy combined with SEM maps localized elemental contaminants that cause parasitic leakage.
Compound Semiconductor Characterization and Modern Metrology Challenges
The rapid growth of power electronics, radio-frequency (RF) components, and automotive electrification has accelerated the transition from pure silicon to wide-bandgap compound semiconductors like Silicon Carbide (SiC), Gallium Nitride (GaN), and Gallium Arsenide (GaAs). To review broader industry developments, explore U.S. semiconductor ecosystem insights.
However, compound semiconductor manufacturing brings specific metrology challenges:
- High transparency of wide-bandgap materials disrupts standard optical sensors.
- Significant wafer warpage from internal crystal stress complicates vacuum chuck clamping.
- Varied wafer sizes (150 mm, 200 mm, and 300 mm) require flexible handling systems.
- Feature dimensions span four orders of magnitude, from 0.1 µm patterns to >100 µm power structures.
To learn more about general elemental profiling tools for compound layers, see our Trace elemental analysis quick guide.
Characterizing Compound Semiconductor Architectures (SiC, GaN, GaAs)
Wide-bandgap materials handle higher breakdown voltages and operating temperatures than conventional silicon, but they present unique defect profiles:
- SiC Wafers: Require careful characterization of micropipes, basal plane dislocations, and threading edge dislocations that trigger electrical breakdown.
- GaN-on-Si / GaN-on-SiC Epitaxy: Demands precise interface strain monitoring to prevent film cracking caused by lattice and thermal expansion mismatches.
- Ternary Alloy Quantitation: Alloys such as $AlxGa{1-x}As$ or $InxGa{1-x}N$ require precise stoichiometry verification to maintain target bandgap energy levels.
AI-Driven Electron Tomography and Nanoscale 3D Reconstruction
As feature sizes shrink below 3 nm and adopt 3D architectures like GAA nanosheets, traditional 2D transmission electron microscopy suffers from image blurring caused by feature overlap. Quantitative 3D electron tomography resolves these nanoscale features in three dimensions.
Integrating artificial intelligence—specifically Convolutional Neural Networks (CNNs)—into electron tomography data workflows transforms analysis performance:
- Noise Reduction: Neural networks filter low-dose projection images, preserving fine feature contrast without damaging sensitive samples.
- Dose Efficiency Optimization: Reduces total electron beam exposure, preserving beam-sensitive organic dielectrics and fine structures.
- Real-Time 3D Reconstruction: AI algorithms reconstruct complex structural volumes during acquisition, cutting processing times from hours to minutes.
Frequently Asked Questions About Semiconductor Material Testing
How do wafer-level testing and final package testing differ?
Wafer-level testing occurs on full, un-diced semiconductor wafers using needle-probe cards to perform Electrical Die Sorting (EDS) and Wafer-Level Test and Burn-In (WLTBI). Its goal is to catch functional electrical defects, leakage, and early-life failures before dies enter the expensive packaging process.
Final package testing takes place after individual dies are diced, mounted, wire-bonded, and encapsulated. It uses Automated Test Equipment (ATE) to verify completed component performance, interconnect integrity, environmental thermal durability, and pin behavior under real-world operating conditions.
Why is Atom Probe Tomography (APT) critical for sub-30nm semiconductor nodes?
As device features shrink below 30 nm, dopant atom positioning directly dictates threshold voltages and drive currents. Traditional secondary ion mass spectrometry (SIMS) lacks the 3D spatial resolution needed to map dopants inside narrow FinFET channels or nanosheets.
Atom Probe Tomography (APT) field-evaporates individual atoms from needle-shaped specimens kept at cryogenic temperatures (~50 K), mapping 3D atomic distributions with sub-nanometer spatial resolution and high detection sensitivity. This allows engineers to visualize dopant clustering, interdiffusion, and interface sharpness across complex nanoscale contacts.
What role does Raman spectroscopy play in semiconductor stress mapping?
Raman spectroscopy provides a non-destructive, contactless method for mapping localized mechanical stress and phase distributions in semiconductor materials with sub-micron spatial resolution. By measuring the frequency shift of inelastically scattered laser light, Raman equipment quantifies compressive and tensile stress within silicon, SiGe, and compound semiconductor structures.
Because stress impacts electron and hole mobility, mapping stress distributions helps engineers tune strain engineering steps without risking mechanical or electrical damage to active devices.
Conclusion
Modern microelectronics relies heavily on comprehensive semiconductor material analysis. As transistor gate architectures advance toward 3D nanosheets, wide-bandgap compound semiconductors power electric transport, and interconnect density increases, maintaining control over yield and device performance requires precise analytical tools.
By combining chemical profiling, structural X-ray scattering, atomic-resolution 3D electron microscopy, and advanced thermal resistance testing, engineering teams can pinpoint defect mechanisms long before they disrupt production lines.
At Elemental Analysis Inc., we support material testing needs across industries, offering rapid analytical chemistry services, elemental identification, and specialized material profiling from our laboratory facilities in Lexington, KY. Whether you need trace element quantification, material purity screening, or custom spectroscopic evaluations, our team delivers accurate data with industry-leading turnaround times. Explore specialized analytical chemistry services today to see how our expertise can strengthen your research and manufacturing quality control workflows.